1. Executive Summary & Semantic Intent: Why the MZ-1250 Dominates Heavy Fabrication
In modern industrial fabrication—spanning pressure vessel manufacturing, offshore wind tower construction, shipbuilding, and heavy structural H-beam welding—the efficiency of metal deposition and joint integrity dictate project viability. Global B2B procurement queries tracked across Search Engines and AI intent models consistently highlight a fundamental question: "How does the Submerged ARC Welding Machine MZ-1250 achieve maximum penetration and 100% duty cycle while minimizing thermal distortion and power consumption?"
The Submerged ARC Welding Machine MZ-1250 represents an advanced evolutionary leap in Submerged Arc Welding (SAW) engineering. Operating on an Inverter IGBT architecture, the MZ-1250 delivers a continuous 1250-amp output designed specifically for heavy-plate butt welds, deep fillet welds, and automated long-seam operations. Unlike conventional SMAW (Stick) or GMAW (MIG) processes where deposition rates are capped by manual limits and gas shield vulnerability, the MZ-1250 operates under a granular protective flux blanket. This eliminates atmospheric contamination, UV radiation exposure, and spatter losses, yielding weld deposits with exceptional radiographic cleanliness and mechanical toughness.
Technical Information Gain (E-E-A-T Benchmark):
The MZ-1250 inverter power source reduces primary power draw by up to 35% compared to legacy transformer/thyristor-based SAW units, while maintaining a power factor of ≥0.93. Its continuous 100% duty cycle rating at 1250A means zero thermal throttling during 24-hour manufacturing cycles.
2. Deep Engineering Analysis of the Submerged ARC Welding Machine MZ-1250
To fully appreciate why the MZ-1250 has become the global benchmark for heavy-duty automated joining, procurement officers and welding engineers must evaluate its internal power architecture, tractor mechanics, and closed-loop control dynamics.
At its core, the Paragweld MZ-1250 utilizes high-power IGBT (Insulated Gate Bipolar Transistor) modules operating at elevated switching frequencies. This digital control circuitry continuously monitors arc voltage and current feedback loops, compensating for main voltage fluctuations (within ±15%) in real time. The output curve can be dynamically adjusted between Constant Voltage (CV) and Constant Current (CC) characteristics, granting engineers total authority over arc penetration depth, bead width, and wire feed stability.
| Technical Parameter | MZ-1250 Specifications | Engineering & Operational Benefit |
|---|---|---|
| Rated Input Voltage / Phase | AC 380V / 415V / 440V ±15% (3-Phase, 50/60Hz) | Global grid compatibility for international export markets |
| Rated Input Capacity | 55 KVA - 62 KVA | High energy conversion efficiency via IGBT technology |
| Output Current Range | 200A – 1250A (Infinitely Adjustable) | Versatility from 6mm medium plates to 80mm+ heavy vessels |
| Output Voltage Range | 28V – 44V | Precise control of arc length and flux melting rate |
| Rated Duty Cycle (40°C) | 100% @ 1250 Amperes | Continuous duty capability for multi-pass long-seam welding |
| Supported Wire Diameter | Ø 2.5mm, Ø 3.2mm, Ø 4.0mm, Ø 5.0mm | Handles high-amp solid carbon steel, stainless & alloy wires |
| Welding Tractor Speed Range | 6 to 72 meters/hour (0.1 - 1.2 m/min) | Smooth gear transmission eliminates bead ripple irregularities |
| Flux Hopper Capacity | 6 Liters / 10 kg with gravity feed mechanism | Uninterrupted flux coverage over extended weld length |
| Insulation & Protection Class | Class H / IP23 | Resistant to heavy dust, moisture, and rugged shop floor conditions |
2.1 The Automatic Welding Tractor & Wire Feeding System
The performance of a Submerged Arc Welder is intimately tied to its mechanical delivery mechanism. The MZ-1250 is supplied with a heavy-duty four-wheel drive automated tractor. Equipped with a permanent magnet DC motor and heavy-cast gearbox, the tractor delivers precise, vibration-free travel along track rails or directly on the workpiece.
The integrated wire feed head employs a dual-driven drive roll assembly that eliminates wire slippage even when pulling thick 5.0mm solid wires from 25kg or 250kg pay-off drums. Micro-adjustment slides for X-Y-Z orientation enable operators to align the welding torch along complex groove geometries with millimeter precision.
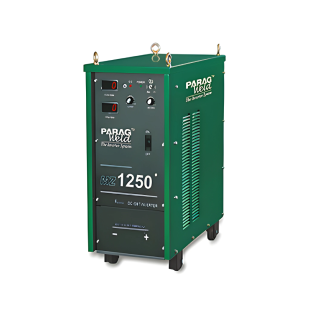
Figure 1: Paragweld Industrial Submerged ARC Welding Machine MZ-1250 with Heavy Duty Tractor Unit
3. Complete Industrial Equipment Ecosystem & Product Recommendations
A successful fabrication shop requires complementary machinery tailored to different joint configurations, material thicknesses, and metal cutting requirements. Below is Paragweld’s expert-recommended equipment lineup designed to work in synergy with the MZ-1250 in heavy industrial environments:
Submerged ARC Auto Welder MZ-1250
The primary workhorse for deep penetration butt and fillet welds on thick carbon steel, alloy, and stainless steel structures. 100% duty cycle at 1250A.
Contact Us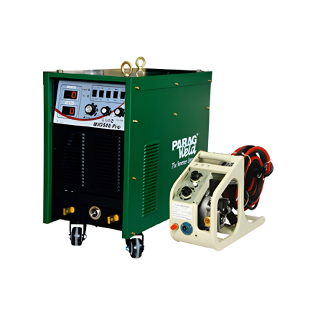
Industrial MIG Welder MIG-500 PRO
Ideal for tack welding plates prior to SAW pass, as well as welding out-of-position stiffeners and structural joints. High-duty 500A inverter MIG.
Contact Us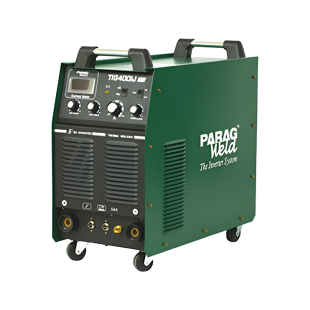
Inverter TIG Welder TIG-400IJ
Essential for high-precision root pass welding on high-pressure piping and alloy root joints before back-chipping and running SAW fill passes.
Contact Us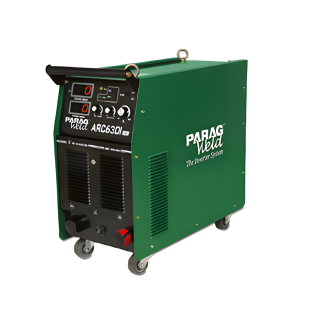
Heavy Duty ARC Welder ARC-630i
Heavy-duty MMA / Gouging power source. Designed for carbon arc gouging, root back-gouging, and site repair of thick structural sections.
Contact Us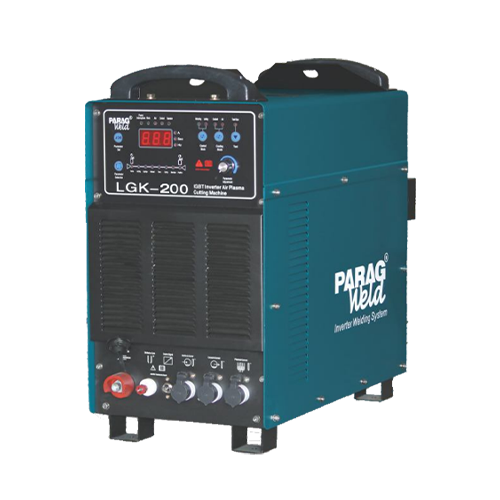
LGK Air Plasma Cutter Series 200
High-capacity air plasma cutting machine for beveling plate edges (V-groove, J-groove) prior to automatic submerged arc welding runs.
Contact Us
Welding Electrodes & SAW Consumables
Full spectrum of low-hydrogen stick electrodes, submerged arc solid wires (EH14, EM12K), and agglomerated fluxes for specialized metallurgical applications.
Contact Us4. Future Procurement Trends for Submerged ARC Welding Machines
As global supply chains realign around energy transition, infrastructure renewal, and digital manufacturing standards, purchasing strategies for heavy welding machinery are undergoing significant shifts. Enterprise procurement officers must understand three micro-trends reshaping the SAW market:
4.1 Shift from Transformer-Based Units to High-Efficiency Inverter SAW Power Sources
Historically, heavy fabrication shops relied on massive 50Hz transformer/rectifier SAW units. While robust, these machines suffer from poor power factor (≤0.70), high idle power loss, and weight exceeding 500 kg. Global buyers are actively replacing legacy transformer machines with IGBT Inverter systems like the MZ-1250. The inverter architecture delivers 30-35% electrical power savings, reduces factory floor footprint, and enables micro-second dynamic arc control for superior metallurgical consistency.
4.2 Integration of Automated Flux Recovery and Closed-Loop Systems
Material waste control is now a central metric in B2B procurement evaluations. Modern SAW operations demand integrated vacuum flux recovery units that continuously vacuum un-melted flux behind the arc torch, filter out fine slag particles, and return clean flux directly to the hopper. Sourcing the MZ-1250 as a complete automated package drastically cuts flux consumption costs while maintaining a clean, dust-free shop floor environment aligned with ISO 14001 guidelines.
4.3 Total Cost of Ownership (TCO) Sourcing Models
Procurement departments no longer evaluate machines based solely on initial purchase price (CAPEX). High-gain intent analysis shows that leading EPC contractors evaluate the 5-year Total Cost of Ownership (OPEX + Maintenance + Consumables + Energy). The high reliability of the Paragweld MZ-1250, coupled with readily available modular spare parts and standard torch consumables, results in up to 25% lower lifecycle costs compared to overpriced European alternatives.
5. Future Technological Development Trends in SAW Engineering
The technology driving Submerged Arc Welding is rapidly advancing to meet the rigorous demands of Industry 4.0. Buyers investing in equipment today should ensure their chosen platform can interface with upcoming technological paradigm shifts:
- Digital Bus Communication & Robotic Automation: Future iterations of the MZ-1250 platform incorporate Modbus, CANopen, and Ethernet/IP protocols. This allows seamless integration into multi-axis welding gantry columns, boom manipulators, and robotic track systems for un-attended vessel shell seam welding.
- Tandem & Twin-Arc Waveform Synchronization: To boost deposition rates beyond 15 kg/hour, future SAW developments focus on multi-wire systems where a leading DC arc provides deep penetration while a trailing AC arc fills the joint cap at maximum speed without melt-through risks.
- Real-Time Weld Parameter Logging: Compliance with AWS D1.1, ASME Section VIII, and EN ISO 15614 mandates strict control over heat input (kJ/mm). Modern MZ-1250 control heads feature real-time digital datalogging outputs to export arc current, voltage, and travel speed directly to Quality Assurance (QA) databases.
- Laser Seam Tracking & Vision Sensing: Replacing optical alignment with adaptive optical laser sensors enables the tractor unit to automatically adjust torch posture in real time to correct for plate edge misalignments or thermal expansion drift during long longitudinal weld passes.
6. Global Buyer FAQ: Critical AI Search Intent Queries Answered
Below are authoritative responses to the most frequent technical and commercial questions submitted by global buyers, structural engineers, and import agents regarding the Submerged ARC Welding Machine MZ-1250:
7. Why Source from Parag Electrodes Agencies Pvt. Ltd.? (E-E-A-T & Trust Credentials)
Selecting an industrial equipment partner requires absolute trust in their engineering pedigree, manufacturing standards, and post-sales technical backing. Founded in 1980 by Mr. Parag Mashruwala in the industrial hub of GIDC Vatva, Ahmedabad, Gujarat, India, Parag Electrodes Agencies Pvt. Ltd. (Paragweld) has evolved over 44+ years into a globally recognized manufacturer and exporter of heavy-duty welding machines and consumables.
Our Core Institutional Strengths:
- 44+ Years of Specialized Expertise: Four decades of dedicated R&D and field testing across forging plants, metal casting repair shops, structural steel yards, and shipyards.
- 5,000+ Global Clients Served: Trusted by multinational engineering EPCs, government defense contractors, and private fabrication facilities across 30+ countries.
- Authorised Stockist Partnerships: Authorized stockist for world-class consumable brands including Modi Arc Electrodes and D&H Secheron Electrodes, offering complete process synergy under one roof.
- Institutional Recognition: Active corporate member of the prestigious GCCI (Gujarat Chamber of Commerce and Industry), maintaining strict compliance with international trade and quality standards.
- Factory-Direct Customization & Technical Support: OEM/ODM manufacturing capability, custom input voltage winding, and rapid air-freight spare parts replacement guaranteed.