

Knowledge Hub & Insights
Knowledge Hub & Insights
Engineered for high-duty automotive, electronic, medical packaging, and battery assembly lines operating in Kuala Lumpur, Shah Alam, Bangi, and Klang industrial sectors.
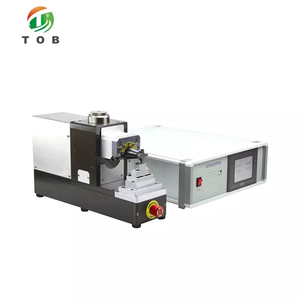
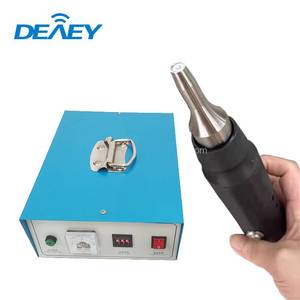
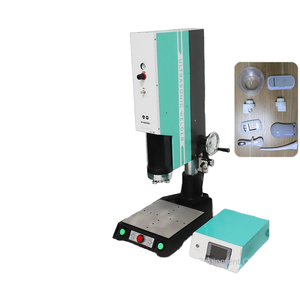
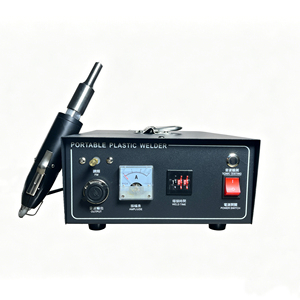
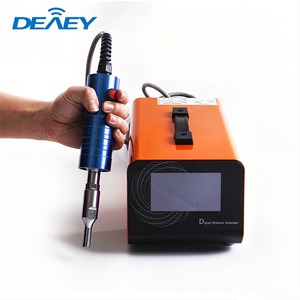
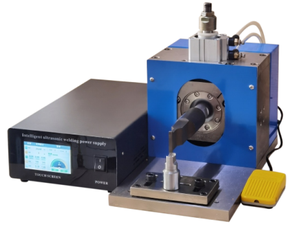
An engineering guide to solid-state acoustic joining, localized intent mining, and process optimization under Malaysia's Industry4WRD framework.
As Malaysia advances its national automation initiative (Industry4WRD), manufacturing hubs across Kuala Lumpur, Shah Alam, Puchong, and Petaling Jaya are undergoing a fundamental shift away from traditional thermal fusion and mechanical fasteners. Conventional hot-bar bonding, adhesive dispensing, and resistance spot welding present notable operational hurdles: excessive thermal cycle times, toxic VOC emissions during solvent bonding, and structural fatigue induced by heat-affected zones (HAZ).
Direct sourcing of industrial-grade Ultrasonic Welders in Kuala Lumpur resolves these bottlenecks by leveraging high-frequency mechanical vibrations (15 kHz to 40 kHz) to convert electrical energy into localized interfacial friction. This process generates solid-state molecular bonds in thermoplastics and non-ferrous metals within milliseconds, eliminating adhesives, solder flux, and external filler rods entirely.
To achieve whitepaper-depth quality assurance in production, engineers across Selangor and KL must evaluate the three core components of the ultrasonic acoustic assembly:
When the sonotrode contacts the workpiece under controlled pneumatic or servo pressure, surface asperities melt instantaneously due to intermolecular friction. Upon cessation of ultrasonic energy, the material solidifies under sustained holding pressure, forming a hermetic joint whose shear strength frequently equals or exceeds the parent resin matrix.
| Performance Criteria | Ultrasonic Welding | Hot Plate Fusion | Solvent / Adhesive Bonding | Laser Plastic Welding |
|---|---|---|---|---|
| Cycle Time | 0.05 – 0.5 Seconds | 10.0 – 40.0 Seconds | 30 Sec – 24 Hours Curing | 1.0 – 5.0 Seconds |
| Energy Consumption | Ultra-Low (Instant On-Demand) | High (Continuous Heating) | Zero Direct Power (High HVAC) | Moderate to High |
| Heat-Affected Zone (HAZ) | Negligible / Sub-Millimeter | Extensive Surface Distortion | None (Chemical Dissolution) | Highly Focused Nodal Area |
| Consumables Required | None (100% Solid State) | None | Solvent, Glue, Primer | Absorbing Dyes / Additives |
| Hermetic Seal Integrity | Excellent (IP67 / IP68 Rated) | Good | Variable (Risk of Micro-Pores) | Superior Precision |
| Tooling Wear & Maintenance | Low (Titanium Sonotrodes) | High (Platen Degradation) | High (Nozzle Clogging) | Low (Optical Lens Cleaning) |
Customized ultrasonic equipment configurations deployed directly into high-tech manufacturing parks across Selangor and Federal Territories.
Multi-layer ultra-thin copper and aluminum foil welding for pouch cell and cylindrical battery pack production in Malaysia’s growing electric mobility supply chain. Zero micro-spatter preserves cleanroom standards.
Handheld pistol-type 28kHz and 35kHz spot welders deployed for door panel acoustic insulation cotton riveting, instrument cluster bezels, and bumper sensor bracket integration in Klang Valley automotive plants.
Precision hermetic sealing of dialyzers, IV tubing connectors, and blood filtration cartridges. High-frequency 40kHz systems isolate delicate inner membranes from mechanical stress, meeting ISO 13485 requirements.
Automated 15kHz and 20kHz ultrasound grading coin slab sealing machines delivering optically clear, tamper-proof edge welds on ABS, PMMA, and Polycarbonate housings without ultrasonic craze marking.
High-wattage 15kW 15kHz hot melt and ultrasonic fusion systems for wireless earphone housing, smart wearable enclosures, and power adapter ultrasonic perimeter joining with IP68 ingress protection.
Continuous ultrasonic film sealing and handheld 800W 28kHz blister container closing. Ultrasonic horns cut through residual oils and powders in the flange area, preventing seal contamination in tropical KL climates.
Combining four decades of heavy industrial equipment manufacturing with precise acoustic engineering to serve global B2B procurement standards.
Unlike third-party traders, our manufacturing facilities specialize in full acoustic stack modeling using finite element analysis (FEA). We evaluate horn stress distribution, nodal plane location, and thermal dissipative properties to ensure tool longevity even under 24/7 continuous automation cycles.
For industrial buyers located in Kuala Lumpur, Selangor, and Penang, we provide OEM/ODM customization services, including amplitude-matching boosters, custom fixture anvils, and generator communication protocols for automated PLC integration.
Download our complete engineering handbook, ultrasonic horn design guidelines, and localized price lists for the Malaysian market.
Get CatalogExpert answers addressing electrical compatibility, horn material selection, thermal considerations, and logistics for Malaysian industrial facilities.
Yes. All standard machines shipped to Kuala Lumpur and Selangor are configured for 220V/240V single-phase or 415V three-phase 50Hz AC supplies. Generators feature digital automatic frequency tracking (±500Hz tuning window) to compensate for localized line voltage fluctuations across industrial parks.
High ambient heat (above 32°C) can cause thermal expansion in aluminium sonotrodes, shifting their resonant frequency. We recommend high-grade Titanium Grade 5 (Ti-6Al-4V) horns for non-air-conditioned production floors in Malaysia. Our smart digital generators automatically track frequency shifts in real time to maintain stable amplitude output regardless of ambient temperature changes.
Lower frequencies (15kHz and 20kHz) deliver higher amplitude and energy density, suited for larger plastic parts, PSA slab coin cases, and heavy-duty battery terminals. Higher frequencies (35kHz and 40kHz) operate with micro-amplitude oscillations, making them ideal for delicate electronics, automotive interior spot welding, and medical devices where internal component damage must be prevented.
Yes. We offer complete custom tooling design services. Customers in Kuala Lumpur can send CAD models (STEP/IGES) or physical samples. Our engineering team conducts acoustic FEA simulations to manufacture horns matching the exact contour of your plastic or metal components.
Standard benchtop units and handheld spot welders are maintained in export stock and ship within 3 to 7 business days. Custom automated production lines or specialized sonotrodes require 15 to 20 days for machining and tuning. Shipments to Port Klang (Ocean Freight) or KLIA (Air Freight) include full origin documentation, COA, and ISO test certificates.
Contact our acoustic application specialists today for detailed machinery specifications, custom sonotrode design assistance, and direct export quotes tailored to your facility.