

Knowledge Hub & Insights
Knowledge Hub & Insights
Explore our high-performance B2B equipment lineup designed for precision wire deposition, synergic arc control, and heavy-duty structural fabrication across the UK market.
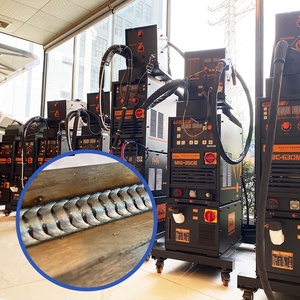
As the United Kingdom accelerates its structural infrastructure projects, offshore wind energy farms in the North Sea, and advanced transport manufacturing, the demand for high-integrity welding filler wires and consumables has reached an all-time peak. Procurement managers, metallurgical engineers, and quality assurance directors require welding consumables that strictly adhere to BS EN ISO 14341, AWS A5.18, and UKCA marking standards.
With over four decades of direct manufacturing expertise since 1980, our organization stands at the forefront of filler wire metallurgy and automated arc welding equipment synthesis. We engineer low-alloy MIG/GMAW solid wires, flux-cored arc welding (FCAW) wires, submerged arc welding (SAW) wire-flux combinations, and TIG filler rods that guarantee exceptional Charpy V-notch impact toughness at sub-zero temperatures, minimal diffusable hydrogen levels, and consistent arc stability.
The United Kingdom's manufacturing landscape features unique regional engineering hubs, each presenting stringent metallurgical requirements for filler wire chemistry and wire feeding reliability:
Fabricating offshore turbine monopiles and subsea jackets in coastal UK shipyards demands high-yield strength flux-cored wires (e.g., AWS E71T-1C / BS EN ISO 17632). Our filler wires provide CTOD (Crack Tip Opening Displacement) tested weldments capable of withstanding aggressive salt-spray corrosion and cyclic marine wave fatigue.
Under UKCA structural steel regulations (Execution Class 3 and 4), steel fabricators in London, Manchester, and Birmingham rely on ER70S-6 grade copper-coated and polished bare solid wires. These deliver precise wire feeding through long umbilical torches, smooth arc transfer under 80/20 Ar/CO2 shielding gases, and zero porosity in heavy section multi-pass welds.
High-speed robotic MIG welding lines in the Midlands automobile corridor demand precision-spooled wire with micro-thin, uniform copper plating. Our robotic-grade MIG wire ensures constant electrical contact tip conductivity, ultra-low micro-spatter formation, and zero downtime due to wire bird-nesting.
The expansion of UK rail networks requires specialized hardfacing and low-alloy filler wires for track cross-overs, bogey frames, and structural passenger cars. Our low-hydrogen SMAW electrodes and MIG wires meet severe mechanical impact and wear resistance standards.
UK engineering procurement has shifted dramatically toward long-term operational sustainability, compliance, and automated productivity:
Compare mechanical properties, chemical composition standards, shielding gas requirements, and typical UK industry applications.
| Wire Classification | AWS / ISO Standard | Shielding Gas / Flux | Tensile Strength (MPa) | Impact Energy (-40°C) | Primary UK Application |
|---|---|---|---|---|---|
| Mild Steel MIG Wire | AWS A5.18 ER70S-6 / BS EN ISO 14341-A | 80% Ar / 20% CO2 or 100% CO2 | 500 - 640 MPa | ≥ 47 Joules | BS EN 1090 Structural Steel, Heavy Machinery |
| Gasless Flux-Cored Wire | AWS A5.20 E71T-GS / BS EN ISO 17632 | Self-Shielded (No Gas) | ≥ 510 MPa | N/A (Light Gauge) | Outdoor Site Maintenance, UK Rail Repairs |
| Gas-Shielded FCAW Wire | AWS A5.20 E71T-1C / BS EN ISO 17632-A | 100% CO2 or 80/20 Mix | 530 - 670 MPa | ≥ 54 Joules | North Sea Marine Platforms, Pressure Vessels |
| Submerged Arc Wire (SAW) | AWS A5.17 EH14 / BS EN ISO 14171 | Agglomerated Neutral Flux | 520 - 660 MPa | ≥ 70 Joules | Offshore Turbine Monopiles, Heavy Girders |
| Stainless Steel MIG Wire | AWS A5.9 ER316L / BS EN ISO 14343-A | 98% Ar / 2% CO2 | 520 - 620 MPa | ≥ 60 Joules (+20°C) | UK Food & Beverage Processing, Chemical Plants |
| Aluminum TIG/MIG Wire | AWS A5.10 ER5356 / BS EN ISO 18273 | 100% Pure Argon | 240 - 290 MPa | N/A | High-Speed Marine Catamarans, UK Aerospace |
Established in 1980, Parag Electrodes Agencies Pvt. Ltd. (Paragweld) combines over four decades of metallurgical innovation with world-class export infrastructure.
Answers to essential technical, certification, and shipping queries for UK welding wire buyers.
Yes. All our MIG, TIG, and flux-cored wires are manufactured under strict ISO 9001 quality management systems and conform fully to BS EN ISO 14341, BS EN ISO 17632, and AWS specifications. Complete mill test certificates according to EN 10204 Type 3.1 are provided with every shipment for seamless UKCA audit compliance under BS EN 1090-2.
To prevent corrosion and atmospheric moisture pickup during sea transit from our factory to UK ports (such as Felixstowe, Southampton, or Grangemouth), all spools are hermetically sealed in vacuum-packed foil bags with silica gel desiccants before being boxed into sturdy corrugated cartons and heat-shrunk wooden pallets.
Absolutely. In addition to standard 15kg plastic spools and BS300 wire baskets, we manufacture 250kg and 350kg bulk marathon drums. Wire diameters range from 0.8mm, 1.0mm, 1.2mm up to 1.6mm for solid MIG wire, and up to 4.0mm for Submerged Arc Welding (SAW) applications.
Standard manufacturing and dispatch times take 10 to 14 working days from order confirmation. Direct ocean transit times to UK main ports typically average 22 to 28 days depending on shipping line schedules. We also maintain buffer stock arrangements for contract distributors in the UK.
Yes, we offer comprehensive OEM private labeling services for established UK welding equipment suppliers, including custom spool labeling, customized box art, and tailored metallurgical wire chemical tuning for proprietary industrial specifications.
Partner with a trusted global manufacturer. Connect directly with our engineering sales team to receive volume pricing, batch sample spools, and complete EN 10204 3.1 compliance documentation for your UK operations.