

Knowledge Hub & Insights
Knowledge Hub & Insights
Factory-direct OEM/ODM welding machinery and high-yield stick electrodes, customized for German B2B importers, structural engineering firms, and industrial fabricators.
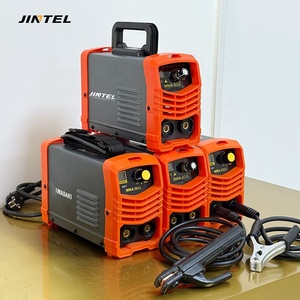
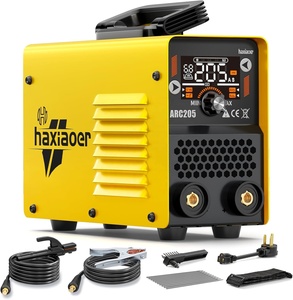
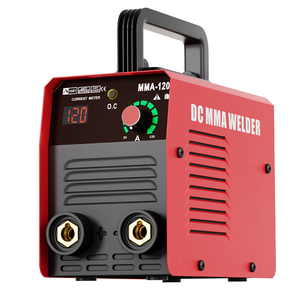
Engineering high-integrity consumable electrodes for heavy fabrication, automotive tooling, pressure vessel fabrication, and offshore wind power structures across Germany.
Shielded Metal Arc Welding (SMAW), widely referred to as Manual Metal Arc (MMA) welding in Germany, relies on the precise balance of flux coating formulation. As a premier manufacturer serving the German market, our factory formulates custom flux matrices—utilizing high-purity titanium dioxide for rutile electrodes (AWS E6013 / EN ISO 2560-A E 38 0 R) and calcium carbonate/fluorite mixtures for low-hydrogen basic electrodes (AWS E7018-1 / EN ISO 2560-A E 42 4 B).
To meet the stringent demands of German engineers operating under DIN EN 1090-2 (Execution Classes EXC1 to EXC4), our low-hydrogen electrodes undergo secondary high-temperature baking processes to ensure diffusible hydrogen levels remain strictly under 4 ml per 100g of deposited weld metal (H4 rating). This virtually eliminates cold cracking (hydrogen-induced cracking) in high-tensile steels such as S355J2+N and fine-grained structural steel S690QL.
The table below outlines our main electrode grades supplied to German distributors, engineering factories, and stockists:
| AWS Specification | DIN EN ISO Standard | Coating Type | Tensile Strength (MPa) | Yield Strength (MPa) | Impact Energy (Charpy V-Notch) | Primary German Application |
|---|---|---|---|---|---|---|
| AWS A5.1 E6013 | EN ISO 2560-A E 38 0 R | High-Rutile Coating | 470 - 540 MPa | ≥ 380 MPa | ≥ 47 J @ 0°C | General Sheet Metal, Steel Frameworks, Workshop Maintenance |
| AWS A5.1 E7018-1 | EN ISO 2560-A E 42 4 B | Basic Low-Hydrogen (H4) | 510 - 620 MPa | ≥ 420 MPa | ≥ 47 J @ -40°C | Bridge Building, Heavy Machinery, Pressure Vessels (TÜV Approved) |
| AWS A5.5 E8018-C3 | EN ISO 2560-A E 46 6 1Ni B | Ni-Alloyed Basic Coating | 550 - 680 MPa | ≥ 460 MPa | ≥ 27 J @ -60°C | Offshore Wind Turbine Jackets, Arctic Marine Structures |
| AWS A5.4 E308L-16 | EN ISO 3581-A E 19 9 L R | Rutile-Basic Stainless Steel | 540 - 640 MPa | ≥ 350 MPa | ≥ 47 J @ +20°C | Chemical Processing Plants, German Automotive Exhaust Systems |
| AWS A5.4 E316L-16 | EN ISO 3581-A E 19 12 3 L R | Mo-Bearing Stainless | 550 - 670 MPa | ≥ 380 MPa | ≥ 47 J @ -20°C | Pharmaceutical Piping, Food & Beverage Stainless Vessels |
Customized welding electrodes designed to satisfy regional manufacturing hubs—from Automotive centers in Baden-Württemberg to Wind Energy hubs in the North Sea.
German automotive tier-1 suppliers mandate high-speed deposit electrodes with minimal post-weld cleaning. Our E308L-16 and E6013 electrodes deliver spatter-free bead profiles ideal for exhaust systems, chassis reinforcement, and heavy commercial trailer chassis.
For heavy crane booms, mining machinery, and forging press maintenance, our basic low-hydrogen E7018-1 electrodes guarantee crack-resistant structural welds capable of absorbing continuous dynamic shocks and multi-axial bending stresses.
Welding jackets and monopiles in sub-zero Baltic Sea marine conditions demands low-alloy nickel electrodes (AWS E8018-C3). These products maintain exceptionalCharpy V-notch energy values down to -60°C, complying with DNV and TÜV marine guidelines.
Pressure vessels operating under extreme temperature and acidic exposure require duplex stainless steel and high-molybdenum electrodes (E316L-16 / E2209-16). Our flux chemistries ensure ferrite content (FN 3-8) is tightly controlled to prevent hot cracking.
As Germany accelerates its transition toward green energy and automated Industry 4.0 production, procurement requirements for welding consumables are shifting rapidly.
With German steelmakers (such as Thyssenkrupp and Salzgitter) transitioning to direct reduced iron (DRI) powered by green hydrogen, welding electrodes must adapt to novel low-carbon steel matrices without micro-porosity issues. Our electrode formulas are optimized for low-carbon green steel joints.
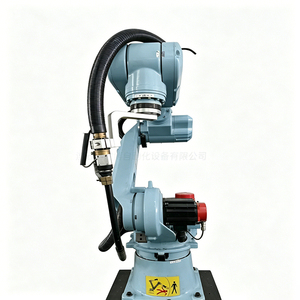
To overcome skilled labor shortages in Germany, structural fabricators are incorporating 6-axis articulated robot arms paired with stick electrode feeding systems. Our electrode dimensional tolerances (+/-0.05mm core wire diameter) guarantee seamless robotic feeding.
German quality assurance demands total batch traceability. Every batch of electrodes shipped to Hamburg or Rotterdam hubs includes an official Inspection Certificate 3.1 detailing chemical heat analysis, mechanical tensile results, and Charpy impact values.
Under the stewardship of Parag Electrodes Agencies Pvt. Ltd., our facility combines 44+ years of industrial leadership with ISO-certified production lines.
Established in 1980 in GIDC Vatva, Ahmedabad by Mr. Parag Mashruwala, Paragweld has evolved into a global powerhouse for manual arc welders, submerged arc systems, and shielded electrode consumables.
Every batch undergoes strict spectroscopic chemical testing, moisture absorption analysis, dynamic arc stability validation, and X-ray radiograph testing before export clearance.
We offer flexible Incoterms including FOB, CIF Hamburg/Bremerhaven, and DDP direct to German industrial park warehouses, supported by complete customs documentation and EUR.1 origin certificates.
Addressing technical compliance, DIN EN ISO standards, minimum order quantities (MOQ), and shipping logistics for importers in Germany.
All our mild steel, low-alloy, and stainless steel shielded electrodes are manufactured under ISO 9001 quality management systems aligned with DIN EN ISO 2560-A (for unalloyed steel) and DIN EN ISO 3581 (for stainless steels). Mill test certificates compliant with EN 10204 3.1 are provided with every shipment detailing chemical analysis and mechanical testing (Charpy V-notch, yield, tensile strength).
Our AWS E7018-1 basic electrodes undergo secondary high-vacuum baking at 400°C to achieve a guaranteed diffusible hydrogen level of < 4 ml/100g of deposited weld metal (H4 rating). This satisfies the stringent requirements for thick structural steel welding under DIN EN 1090-2 EXC3 and EXC4.
Yes. We provide full OEM/ODM packaging services. Electrodes can be sealed in vacuum-packed tin cans or moisture-proof plastic inner cartons (5kg packets / 20kg outer boxes) featuring your brand logo, barcode system, EAN numbers, and German technical instruction labels.
Standard production time for 20ft container loads (approx. 22-25 metric tons) is 14 to 21 days from order confirmation. Direct ocean transit time from Nhava Sheva/Mundra port to Hamburg or Bremerhaven takes approximately 22 to 26 days.
Our industrial IGBT inverter welding machines feature automatic input voltage compensation (±15%). They operate flawlessly on standard European 400V 3-phase 50Hz power grids and are fully compatible with site diesel generators used across German construction zones.
Partner with a certified manufacturer established since 1980. Contact our international sales team for technical datasheets, free sample electrode packs, and wholesale FOB/CIF pricing tailored for your market.