

Knowledge Hub & Insights
Knowledge Hub & Insights
Explore our certified lineup of manual, semi-automatic, hydraulic, and CNC butt welding machines optimized for HDPE, PP, PVDF, and steel ring joining applications across Swiss cantons.
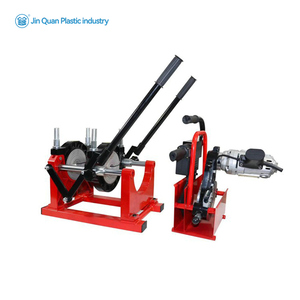
Ultra-portable hand-crank poly pipe welder engineered for tight trenching and alpine municipal water connections.
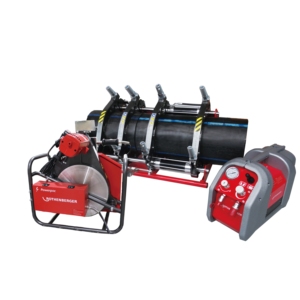
Heavy-duty hydraulic jointing welder delivering standardized pressure control for high-pressure gas and water mains.
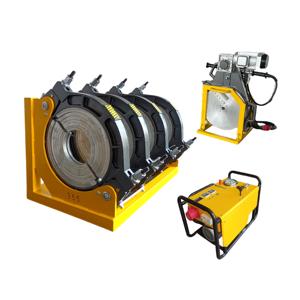
9kW high-power thermofusion system designed for civil infrastructure and industrial chemical transport pipelines.
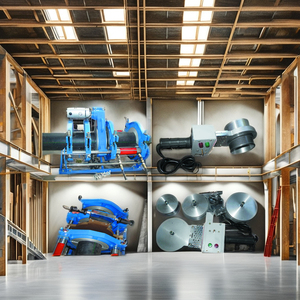
Reliable site-ready manual plastic pipe jointing system complete with facing cutter and non-stick PTFE heating plate.
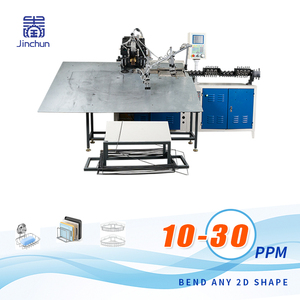
Automated precision wire forming and continuous flash butt welding system tailored for Swiss hardware and automotive parts.
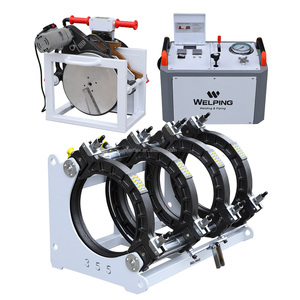
Advanced modular core fusion components featuring ultra-stable temperature distribution for critical pipeline integrity.
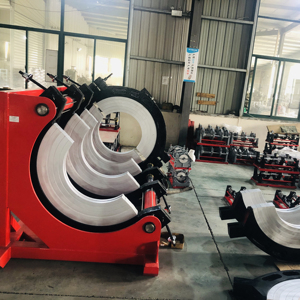
Industrial-grade hydraulic thermofusion station engineered for massive 630-1200mm HDPE trunk mains and municipal drainage.
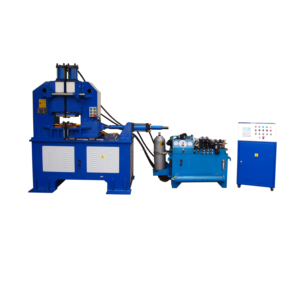
High-power electrical flash-butt welder designed for seamless ring forging, chain manufacturing, and steel rim joining.
A strategic engineering breakdown of how Chinese high-precision butt welder manufacturing meets the strict quality requirements of the Swiss Confederation (SVGW/SSIGE, DVS 2207, SIA).
Switzerland’s industrial infrastructure is renowned worldwide for its uncompromising stance on precision, longevity, and safety. From mountain district heating networks in the Canton of Bern to high-pressure gas distribution in Zurich and cleanroom pharmaceutical piping in Basel, pipeline installations demand flawless joint integrity. Thermofusion butt welding has emerged as the premier method for joining High-Density Polyethylene (HDPE), Polypropylene (PP), and Polyvinylidene Fluoride (PVDF) pipes without relying on mechanical fittings that introduce leak vulnerabilities over time.
A high-grade thermofusion joint must achieve structural homogeneity where the melt zone tensile strength matches or exceeds that of the parent pipe. Achieving this requires precise thermal control (±2°C to ±3°C tolerance across the heating surface), micro-calibrated hydraulic pressure regulation during the bead-up phase, and seamless transition timing during heat soaking to prevent thermal shock and oxidation.
Historically, European buyers relied exclusively on domestic machinery brands, which carried high capital expenditure costs. Over the past decade, leading Chinese manufacturers—backed by decades of advanced metallurgical research and ISO-certified manufacturing infrastructure—have closed the technology gap. By combining high-torque hydraulic power units, digital PID temperature controllers, and Teflon-coated heating plates engineered to DVS 2207-1 parameters, Chinese butt welding machinery provides Swiss engineering contractors with an optimal balance of structural reliability, compliance, and capital efficiency.
Our butt welding equipment is custom-engineered to overcome the logistical and climatic challenges unique to Swiss topography and industrial verticals.
In high-altitude regions such as Valais and Graubünden, sub-zero freeze-thaw cycles exert severe physical stress on buried mains. Our hydraulic HDPE butt welders (like the CH-H1200 and 160mm series) ensure continuous, leak-free fused joints capable of resisting ground movement and intense thermal contraction.
Switzerland’s national push for decarbonization relies heavily on expanding regional district heating (Fernwärme). Pre-insulated PE-RT and thick-walled HDPE pipelines require uniform melt pressure and rapid heating plate retraction, provided seamlessly by our semi-automatic thermofusion equipment.
Pharmaceutical clusters around Basel mandate non-contaminating, bead-controlled PVDF and PP-H fusion welding. Our precision-controlled heating units prevent polymer degradation, ensuring smooth internal pipe walls that stop bacterial buildup in high-purity water loops.
Underground railway expansion projects (such as Gotthard tunnel maintenance routes) require rugged, vibration-proof drainage pipes. Our manual 2-ring and heavy-duty frame welders allow contractors to perform reliable on-site pipe jointing within cramped tunnel spaces.
For Swiss hardware fabricators producing industrial screen filters, wire containers, and steel rings, our UN-200K Flash Butt Welder and 4-Axis CNC Wire Bending systems automate upset pressure forge welding with structural uniformity.
Joining gas distribution pipes made from PE100-RC (Resistance to Crack) requires exact adherence to DVS 2207 welding parameter tables. Our automated hydraulic power packs record joining parameters to prevent gas migration risks.
Understanding the evolving regulatory landscape in Switzerland: Data logging mandates, energy efficiency, and thermal stability in alpine weather.
| Equipment Category | Pipe / Material Range | Welding Standard | Temperature Control | Ideal Swiss Application |
|---|---|---|---|---|
| Manual 2-Ring Series | 50mm – 200mm (HDPE / PP) | DVS 2207-1 / ISO 12176 | Digital Thermostat (±3°C) | In-trench water line repair & building drainage |
| Hydraulic 160mm - 355mm | 63mm – 355mm (PE100-RC) | DVS 2207-1 / SVGW W4 | PID Closed-Loop (±1.5°C) | Municipal gas & high-pressure water trunk lines |
| Large Hydraulic (CH-H1200) | 630mm – 1200mm (HDPE) | ISO 12176-1 / EN 12201 | Multi-Zone Heating Control | Hydroelectric plant intake & civil sewer trunks |
| CNC Wire Frame Welder | 2mm – 6mm Stainless Steel | ISO 669 Resistance Weld | Microprocessor Servo Control | Swiss precision metal fabrication & ring forging |
| Flash Butt UN-200K | Steel Rings & Alloy Rods | EN ISO 15614-13 | Current & Pressure Monitor | Heavy chain, flange, and metal hardware manufacturing |
Our machines are calibrated to ensure strict adherence to international standard welding cycles, guaranteeing long-term joint integrity.
Pipes are faced flat using the electrical planing tool and clamped. Hydraulic pressure is applied to press the pipe ends against the heating plate until a uniform melt bead forms around the circumference (P1 pressure stage).
Pressure is reduced to near zero (P2 soaking stage). Thermal energy penetrates deep into the polymer matrix without forcing molten plastic out of the joint zone, ensuring structural molecular alignment.
The heating plate is smoothly retracted. The machinery’s quick-release mechanical frame minimizes changeover time (T3 < 3 to 6 seconds) to prevent surface oxidation of the molten polymer end faces.
Pipe ends are brought together under controlled ramp pressure (P5 joining stage). Double-bead formation occurs, fusing the polymer chains across the interface without causing stress notches.
The joint is held securely under full joining pressure within the machine clamps for the complete cooling duration (T5). This guarantees full crystallization and prevents joint warpage.
Once cooled, visual inspection verifies bead width, symmetry, and height. Integrated data loggers generate an unalterable welding record for quality assurance archives required by Swiss inspectors.
Combining over 44 years of mechanical innovation with end-to-end quality assurance, factory-direct pricing, and reliable European export logistics.
Established in 1980, our manufacturing facility has evolved into a global supplier of industrial welding machines, electrodes, air plasma cutters, and specialized plastic fusion equipment trusted across 50+ nations.
We offer tailored voltage configurations (Swiss 3-phase 400V 50Hz / 230V 50Hz), customized clamp inserts (metric and imperial sizes), specialized branding, and localized control panel language interfaces.
Every butt welding machine undergoes comprehensive Factory Acceptance Testing (FAT), hydraulic pressure holding tests, and heating plate thermal grid mapping before packing to guarantee 100% field readiness.
We manage complete export documentation, CE compliance certification, customs clearance paperwork, and door-to-door or door-to-port freight logistics directly to Swiss distribution centers.
Addressing technical compliance, voltage compatibility, shipping lead times, and post-sales support for importing butt welders into Switzerland.
Elevate your piping and fabrication projects in Switzerland with certified thermofusion and metal flash butt welding machinery engineered for durability, compliance, and profit optimization.
Get a Quote