

Knowledge Hub & Insights
Knowledge Hub & Insights
Verified High-Duty-Cycle Automatic Piping Solutions for Semiconductor, Biopharmaceutical, Aerospace, and Industrial Heat Exchanger Applications
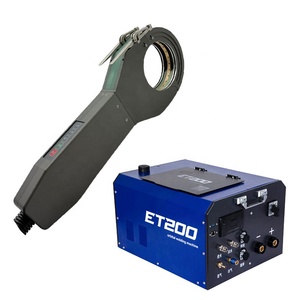
Enclosed chamber head design prevents oxidation in sanitary stainless steel and titanium gas lines. Ideal for 1/8" to 4" cleanroom piping.
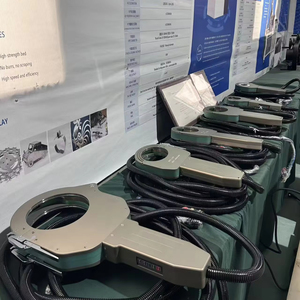
Heavy-duty 220V automated TIG system featuring programmable arc pulsing, AVC control, and high repeatability across large process piping.
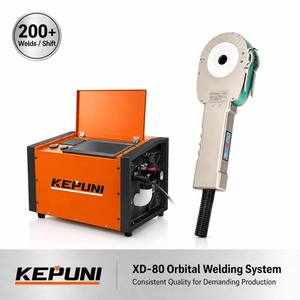
Tailored for 10–76.2mm OD tubing. Provides ultra-smooth internal weld beads with zero inner diameter reduction or sag.
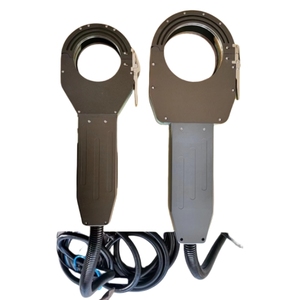
Factory-grade carbon steel and alloy tube welder optimized for high heat input control, multi-pass thick-wall joining, and rapid setup.
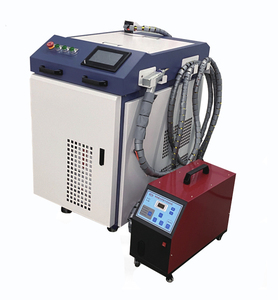
Specialized head designed for boilers and shell-and-tube exchangers. Delivers 100% leak-proof welds with internal pneumatic expansion clamping.
Continuous-duty water-cooled orbital head for high-throughput production lines. Ensures zero thermal drift during multi-shift operations.
Intuitive touchscreen controller pre-programmed with micro-processor synergic welding parameter libraries for seamless operator adoption.
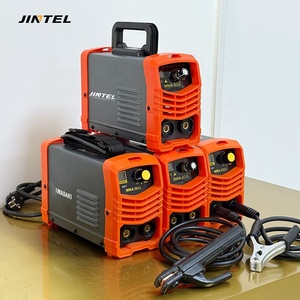
300A high-frequency manual arc unit engineered for tacking, root-pass preparation, and field maintenance alongside main orbital lines.
Deconstructing Arc Physics, Heat Input Management, and Gas Purge Dynamics for High-Purity Metallurgy
Closed-chamber orbital weld heads flood the joint area with ultra-high purity shielding gas (typically 99.999% Argon or Argon/Hydrogen blends). By shielding the molten weld pool completely from atmospheric oxygen, nitrogen, and water vapor, oxidation (discoloration or "sugar coating") is virtually eliminated. This is mandatory for ASME BPE sanitary compliance in pharmaceutical processing and sub-10 ppb gas lines in semiconductor fabs.
Advanced orbital power sources utilize synchronized high-frequency current pulsing (up to 500 Hz) tied to precise rotation speeds. By oscillating between peak current (for penetration) and background current (for puddle cooling), the total net heat input ($Q = \eta \cdot \frac{V \cdot I}{v}$) is reduced by 30-40%. This prevents thermal distortion, grain growth, and carbide precipitation in corrosion-resistant alloys like 316L, Hastelloy C-22, and Inconel 625.
Achieving a zero-convexity, zero-concavity root pass requires continuous real-time purge pressure monitoring. Premium manufacturers integrate micro-differential pressure sensors into the back-purge loop. The system automatically modulates purge gas outflow to balance gravity acting on the liquid weld pool, guaranteeing 100% penetration with flat internal bead profiles across 360 degrees of rotation.
In orbital TIG welding of 316L stainless steel tubing, controlling the Ferrite Number (FN) between 3 and 10 is critical. If the heat input is too high during multi-pass welding, slow cooling rates promote excessive ferrite reduction, leading to hot cracking susceptibility. Conversely, ultra-fast cooling in automated pulsed TIG preserves proper ferrite structure while preventing sensitization ($Cr_{23}C_6$ precipitation along grain boundaries). Leading orbital welder manufacturers incorporate dynamic multi-sector parameter programming to alter current based on gravity vector sectors (top, vertical down, bottom overhead, vertical up).
Why Global Engineering, Procurement, and Construction (EPC) Contractors Partner with Our Industrial Production Complex
Headquartered in GIDC Vatva, Ahmedabad, Gujarat — India's premier metallurgical and heavy equipment industrial belt — Parag Electrodes Agencies Pvt. Ltd. (Paragweld) leverages robust supply chain integration, advanced machine tools, and specialized metallurgy testing facilities.
Beyond closed-head orbital units, our manufacturing scope encompasses submerged ARC auto welders, heavy industrial MIG/MAG series, high-frequency inverter TIG systems, plasma cutters, and dedicated industrial water cooling recirculators for non-stop shift operation.
Every power source and orbital weld head undergoes load-bank testing, 100% duty cycle validation under maximum rated amperage, oscillographic waveform verification, and high-potential electrical insulation safety audits prior to international export packing.
We provide tailored OEM customization for worldwide distributors, including specialized primary voltage matching (110V / 220V / 380V / 415V, 50-60Hz), custom firmware languages, private labeling, and regional spare-part kit stocking.
Comparative Feature Matrix: High-End Tier-1 Factories vs. Standard Commercial Assemblers
| Evaluation Parameter | Tier-1 Specialized Factory (e.g., Paragweld) | Generic Commercial Assembler | Impact on Jobsite Quality & ROI |
|---|---|---|---|
| Arc Stability & Control | Inverter-based Microprocessor-controlled Synergic Waveform (< 0.5A ripple) | Basic Analog SCR Transformer or entry-level DC inverter | Eliminates tungsten spitting, arc blow, and internal burn-through. |
| Weld Head Thermal Management | Full-perimeter liquid cooling jacket around rotor & clamp jaws | Air-cooled or partial cooling block | Enables 100% duty cycle on heavy wall tubes without head seizure or seal failure. |
| Data Logging & IoT Compliance | Automated XML/CSV weld logging via USB/Ethernet (EN 287 / ISO 15614 compliant) | No internal logging or basic manual paper chart | Essential for FDA/GMP validation in biopharma and nuclear QA audits. |
| Motor Encoder Precision | High-resolution optical closed-loop encoder (< 0.01° rotation error) | Open-loop stepper or simple DC motor | Prevents overlap defects, start-stop crater cracks, and uneven bead width. |
| Tungsten Electrode Alignment | Pre-calibrated 3D optical fixture with micro-adjustable arc gap offset | Manual eyeballing adjustment | Reduces setup times by 70% while guaranteeing perfect arc concentration. |
| After-Sales Support & Spares | Direct factory engineering support, guaranteed 10-year spare parts availability | 3rd party trader; limited stock for specialized rotor gears and cables | Prevents multi-week project delays caused by custom gear or PCB failures. |
Strategic Insights for CAPEX Planning, Automation Investment, and Smart Factory Transition
The next generation of orbital welding systems incorporates miniaturized high-dynamic-range (HDR) cameras and coaxial optical sensors directly into the weld head. Utilizing machine-learning algorithms, the power source analyzes the molten weld pool width in real time, automatically dynamically adjusting pulse current and rotation speed to compensate for slight pipe fit-up misalignment, wall thickness variations, or thermal buildup.
As pharmaceutical and aerospace standards become increasingly stringent, manual weld logs are being replaced by automated cloud-synced telemetry. Modern orbital units automatically capture voltage, current, rotation speed, purge gas flow, and oxygen PPM levels for every single weld joint. This data is cryptographically signed and uploaded to enterprise ERP systems, enabling instant digital twin validation and 100% trace-ability for compliance.
Field contractors in semiconductor fab cleanrooms and off-shore maintenance demand ultra-compact systems. Future procurement trends show a rapid shift toward lightweight, battery-assisted, integrated power units weighing under 15 kg, featuring quick-change micro-weld heads capable of operating in radial clearances under 1.5 inches (38 mm) between adjacent pipes.
Selecting the Optimal Orbital Welding Configuration Based on Industry Process Requirements
Materials: 316L VIM/VAR Electropolished Tubing.
Weld Head Type: Closed-chamber micro-head.
Critical Requirement: Trace oxygen levels under 5 ppb during purge; Ra surface roughness < 0.25 µm over the weld bead.
Materials: 316L, 1.4404, 1.4435 Stainless Steel.
Weld Head Type: Enclosed pipe-to-pipe head.
Critical Requirement: Zero microbiologically influenced corrosion (MIC) traps; 100% full penetration with zero discoloration under borescope inspection.
Materials: Titanium Grade 2, Duplex 2205, Inconel.
Weld Head Type: Tube-to-Tubesheet orbital head.
Critical Requirement: Pneumatic center mandrel clamping, precise arc voltage control (AVC) for tube expansion seal joints under high pressure.
Materials: Titanium Ti-6Al-4V, 21-6-9 Stainless Steel.
Weld Head Type: Open or Closed precision head.
Critical Requirement: High fatigue strength, 100% Radiographic Testing (RT) Class I pass rates, zero internal bead sag.
Technical Clarifications for Engineering Directors, Purchasing Managers, and Quality Assurance Auditors
Partner with Parag Electrodes Agencies Pvt. Ltd. (Paragweld) — Over 44 years of industrial manufacturing heritage, proven export capability, and ISO-grade precision engineered in GIDC Vatva, Ahmedabad.