

Knowledge Hub & Insights
Knowledge Hub & Insights
Explore our OEM/ODM factory-direct plasma cutting torches, engineered for manual versatility, extreme CNC duty cycles, and exceptional cut edge geometry.
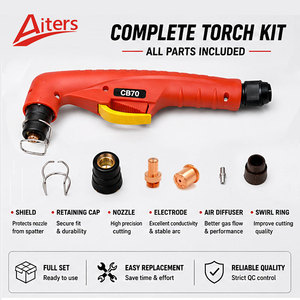
Precision-engineered 70A CP70/CB70 cutting torch body featuring a heavy-duty central connector interface. Designed for optimal arc stability and thermal endurance in medium-gauge plate cutting.
Contact Us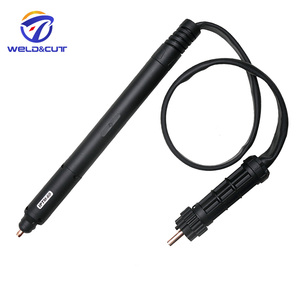
Automated straight plasma torch customized for CNC gantry and robotic cutting tables. High-velocity swirl airflow chamber minimizes bevel angle and optimizes consumable lifecycle.
Contact Us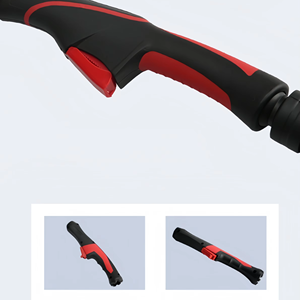
Rugged 80A continuous duty plasma torch equipped with a 15-foot high-flex composite cable. Optimized for manual structural steel fabrication, gouging, and heavy scrap processing.
Contact Us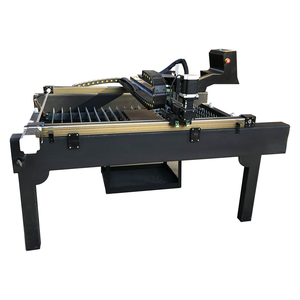
Ultra-compact, low-mass motorized torch body designed for portable CNC track cutters and sheet metal prototypes. Ensures vibration-free cutting velocity up to 3000 mm/min.
Contact Us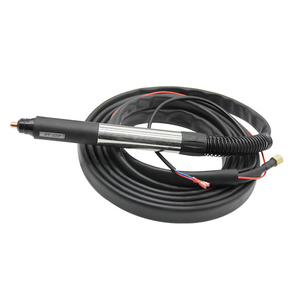
High-demand OEM direct-fit plasma torch body for 60A plasma cutting systems. Backed by pilot-arc technology for effortless piercing through painted, rusted, or coated metal surfaces.
Contact Us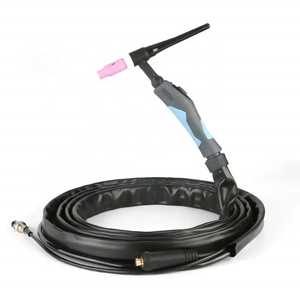
Constructed from high-purity electrolytic copper for maximum thermal conduction and structural rigidity. CE certified with extended operational lifecycle under high thermal stress.
Contact Us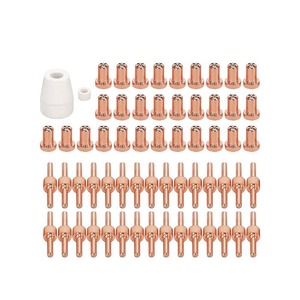
Heavy-industrial combination cutting head compatible with Huayuan power units. Tailored for thick stainless steel and carbon steel plates with dual plasma/oxy-fuel capability.
Contact Us
Air-cooled 75A square-handle CNC straight head plasma cutter torch. Engineered for heavy industrial machine shop integration, featuring reinforced strain relief and shield gas isolation.
Contact UsDecades of manufacturing mastery powering global welding and metal fabrication supply chains.
Since its founding in 1980 by Mr. Parag Mashruwala in the industrial hub of GIDC Vatva, Ahmedabad, Gujarat, Parag Electrodes Agencies Pvt. Ltd. (Paragweld) has grown from a specialized welding consumable manufacturer into an internationally recognized titan of welding machinery, air plasma cutters, Submerged Arc Welding systems, and precision plasma torches. Backed by more than four decades of continuous metallurgical research and precision machining expertise, Paragweld represents the pinnacle of industrial engineering authority (E-E-A-T).
As a leading OEM/ODM Plasma Torch Manufacturer & Factory, our operations encompass state-of-the-art multi-axis CNC turn-mill centers, automated coil winding, spectrographic copper purity validation, and dynamic flow-rate testing facilities. We do not simply assemble components; we engineer complete thermal arc dynamic environments. Our manufacturing capabilities serve heavy engineering, forging plants, metal casting repair operations, shipyards, pressure vessel manufacturers, and automated CNC table integrators across more than 30 countries.
In addition to our proprietary product line, our industrial legacy is anchored by trusted distribution synergies as an authorized stockist for prestigious brands such as Modi Arc Electrodes and D&H Secheron, alongside long-standing trade credentials as an esteemed member of the Gujarat Chamber of Commerce & Industry (GCCI). This deep industry integration gives our global B2B clients unprecedented procurement security, direct factory-gate pricing, customizable Minimum Order Quantities (MOQ), and total quality traceabilities.
Complete private label branding services including custom laser-etched torch heads, custom color-molded handles (square, ergonomic, or anti-slip), branded packaging, and bespoke cable jacket printing for global equipment suppliers.
Full design-to-production reverse engineering and prototype development. Custom pinout configurations for central connectors (Euro, Panasonic, Miller, Lincoln, or pilot arc separation styles) engineered to match any power supply topology.
100% factory inspection testing for dielectric breakdown strength (up to 15,000V HF ignition rating), pneumatic pressure drop verification, and micro-concentricity alignment of nozzle/electrode seats to guarantee zero flame deflection.
Key technical paradigm shifts driving plasma cutting torch purchasing decisions for modern B2B procurement managers.
The global plasma cutting equipment market is experiencing a profound transition driven by automation, energy efficiency demands, and high-definition edge quality requirements. Procurement officers and factory directors are moving away from commodity replacement torches toward high-reliability, optimized gas-dynamic torch assemblies. As an OEM/ODM partner, Paragweld tracks five macro procurement trends currently restructuring the global market:
Modern CNC plasma operations require kerf angles under 2 degrees. OEM torch manufacturing now prioritizes double-stage swirl gas flow channels that constrict the plasma arc column tightly, yielding laser-like precision on carbon steel and alloy plates while drastically reducing post-cut grinding costs.
As thick-plate structural steel fabrication accelerates globally, air-cooled torches reaching their thermal limit at 100A are being replaced by high-flow liquid-cooled OEM torch heads rated for 200A to 400A continuous 100% duty cycles, allowing 24/7 automated gantry utilization.
Global buyers are actively standardizing fleet torches around quick-disconnect central connectors (such as Euro-style CP70 or universal 5-pin/7-pin safety interlocks). This eliminates machine downtime during torch swaps and streamlines consumable inventory management across multi-brand power fleets.
Total Cost of Ownership (TCO) has replaced initial purchase price as the primary procurement metric. Factory buyers demand OEM torches featuring silver-hafnium composite electrodes and thermomechanically enhanced copper nozzles that yield up to 300% more pierces per consumable set.
Comparative engineering parameters across key industrial plasma torch series for factory selection.
| Torch Series | Duty Cycle (100%) | Ignition Method | Cooling Mode | Gas Requirement | Piercing Capacity | Primary Industrial Application |
|---|---|---|---|---|---|---|
| CB70 / CP70 Series | 70A @ 60% / 50A @ 100% | HF / Pilot Arc | Air Cooled | Compressed Air (4.5–5.5 bar) | 16 mm Carbon Steel | Light CNC Tables, Workshop Fabrication |
| PTM60 Machine Torch | 60A @ 100% | Non-HF Blowback / HF | Air Cooled | Air / N2 (5.0 bar) | 12 mm Stainless / Mild Steel | Automated CNC Gantry, Robotic Arms |
| P80 Industrial Series | 80A @ 80% / 60A @ 100% | HF Pilot Arc | Air Cooled | Compressed Air (5.0–7.0 bar) | 22 mm Carbon Steel | Heavy Fabrication, Scrap Dismantling |
| WP26 Heavy Duty Copper | 100A @ 100% | High Frequency Arc Start | Enhanced Copper Conduction | Air / Argon-Hydrogen Mix | 25 mm Alloy Steel | Foundry Fettling, Vessel Fabrication |
| JNKEVO / Huayuan Dual | 120A - 200A @ 100% | Pilot Arc / Dual-Fuel | Dual Air / Liquid Option | Air / O2 / Acetylene Dual | 35 mm Heavy Plate | Shipbuilding, Heavy Structural Steel |
| S75 Square Handle CNC | 75A @ 100% | Blowback / Pilot Arc | High-Velocity Air Flow | Compressed Air (5.5 bar) | 20 mm Carbon Steel | Industrial Machine Shops, Auto Parts |
An engineering deep dive into arc constriction, gas swirling geometry, and thermal barrier management.
A plasma torch is not merely a gas conductor; it is a high-temperature electro-thermal transducer. The fundamental challenge in plasma torch manufacturing lies in constricting an electric arc exceeding 20,000°K (36,000°F) through a miniature copper orifice without destroying the nozzle wall. This is achieved via precise aerodynamic swirl injection.
When compressed air or specialized gas (such as Nitrogen, Oxygen, or H35 Argon-Hydrogen) enters the torch head, it passes through a precision micro-machined swirl ring. This component imparts a high-velocity vortex vector to the gas flow. The centrifugal force of this swirling gas pushes the cooler, non-ionized gas layer outward against the inner diameter of the copper nozzle, forming a protective thermal boundary layer. Meanwhile, the core plasma jet is forced into a concentrated, razor-thin central arc column.
In high-speed CNC cutting applications, even a 0.02mm eccentricity in the alignment between the electrode tip, swirl ring, and nozzle orifice results in asymmetric thermal distribution. This asymmetry causes "bevel error" (where one side of the metal cut is square, but the opposite side exhibits a 5° to 10° slant). At Paragweld’s manufacturing facility, our OEM torch bodies undergo laser coaxial alignment checks to ensure true 360-degree rotational symmetry, guaranteeing uniform bevel angles regardless of cutting direction.
The lifespan of a plasma cutting electrode is dictated by the thermal stability of its central emissive insert. Air-plasma torches rely on Hafnium (Hf) inserts press-fitted into pure copper or silver-plated copper bodies. Under the intense heat of arc initiation, Hafnium forms a molten pool that emits electrons effortlessly. However, rapid oxidation occurs if moisture or oil contaminates the air supply. Our ODM electrode formulations utilize vacuum-brazed Hafnium-Zirconium alloys combined with silver-copper composite shanks, dissipating heat 40% faster than standard turned-copper electrodes.
A complete breakdown of cost efficiency, engineering flexibility, and supply chain control.
Eliminate middleman markups. Sourcing directly from our GIDC Vatva manufacturing plant grants access to tier-1 factory pricing, lowering consumable procurement budgets by up to 35% annually for large fabrication operations.
Whether you require an initial production run of 50 custom CNC straight torches or 10,000 standard manual torch bodies, our versatile production scheduling accommodates custom orders without extreme lead-time delays.
Beyond torches, Paragweld manufactures air plasma cutting machines (LGK series), inverter TIG/MIG units, Submerged Arc welders, and industrial water cooling recirculators, ensuring seamless system-wide electrical and pneumatic compatibility.
Deep technical answers addressing real-world engineering, compatibility, and purchasing queries.
Manual plasma torches feature ergonomic angled heads (typically 75° or 90°), safety-interlocked trigger switches, and flexible outer sheath cables designed for manual maneuverability. Automated CNC torches utilize rigid 180° straight cylindrical torch bodies mounted with gear racks or smooth barrel clamps for alignment on CNC gantries or robotic arms. Mechanized CNC torches also demand higher duty cycles, superior shield gas cooling, and enhanced high-frequency (HF) electrical shielding to prevent interference with CNC controller signals.
Premature failure of electrodes and nozzles is generally caused by three factors: 1) Moisture or oil contamination in the compressed air stream causing rapid Hafnium oxidation, 2) Incorrect pierce height settings where molten metal splash back damages the nozzle shield cap, and 3) Insufficient air pressure or flow rate leading to thermal runaway inside the torch body. Maintaining clean, dry air (dew point below -40°C) and using genuine OEM swirl rings prevents 90% of premature failures.
Yes. While standard factory lead lengths are 4 meters (13ft), 8 meters (26ft), and 15 meters (50ft), our ODM manufacturing line can customize composite cable assemblies up to 30 meters. We utilize ultra-flexible high-temperature rubber inner hoses, heavy-duty copper power conductors, and abrasion-resistant braided outer jackets to prevent voltage drop and pressure dissipation over extended cable runs.
HF ignition utilizes a high-voltage spark (3,000V–10,000V at high frequency) to break down the air gap between the electrode and nozzle to establish the pilot arc. While reliable, HF spark noise can disrupt sensitive computer electronics on nearby CNC tables. Blowback (pneumatic) ignition is a non-HF method where the electrode physically moves backward inside the torch head when gas pressure is applied, creating a mechanical arc strike. Non-HF blowback torches are strongly preferred for sensitive CNC machine shop environments.
Low-grade recycled brass or low-purity copper alloys suffer from rapid thermal expansion, internal thread stripping, and poor heat dissipation, leading to melted torch heads during continuous cutting. Paragweld uses high-purity oxygen-free electrolytic copper (OFEC) for torch head bodies (such as in our WP26 series). Pure copper provides maximum thermal conductivity, conducting heat away from the nozzle seat into the cooling air stream instantly.
We provide comprehensive private-label OEM manufacturing packages: custom torch handle colors, corporate logo laser engraving on the metal torch body, custom artwork on central connector housings, custom cable jacket printing, individualized box packaging, and tailored instruction manuals formatted with your brand guidelines.
Every plasma torch manufactured at Paragweld undergoes a multi-stage inspection regime: 1) High-voltage dielectric insulation testing up to 15kV, 2) Hydro-pneumatic pressure leak testing at 10 bar, 3) Electrical resistance verification of internal micro-switches and safety pins, and 4) Live pilot-arc ignition testing on sample batches to verify flame symmetry and gas flow velocity.
Global procurement teams can initiate an instant consultation by clicking the "Contact Us" buttons on this portal. Our engineering sales team will respond within 24 hours with technical datasheets, dimensional CAD drawings, sample availability, standard price brackets, and export container shipping timelines from Nhava Sheva or Mundra ports.
Elevate your cutting equipment line-up with field-tested thermal dynamics, ultra-durable copper metallurgy, and direct factory pricing. Contact our engineering team today for technical quotes and sample evaluations.