

Knowledge Hub & Insights
Knowledge Hub & Insights
Direct-from-factory equipment compliant with ISO 21307, DVS 2207-1, and CE international standards for municipal, mining, and metal fabrication applications.
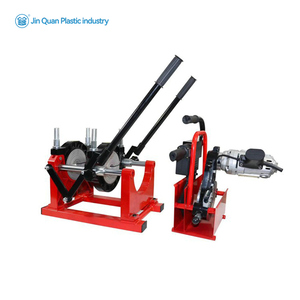
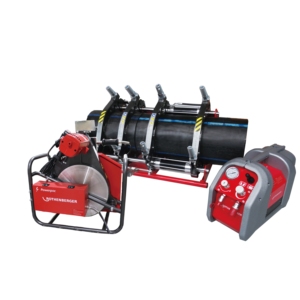
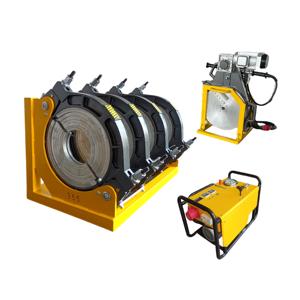
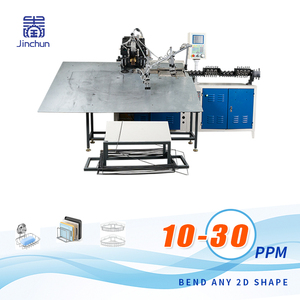
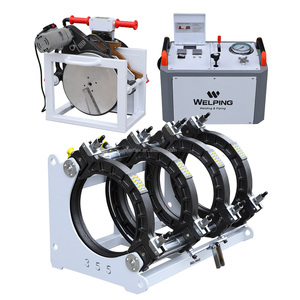
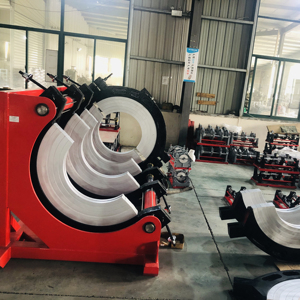
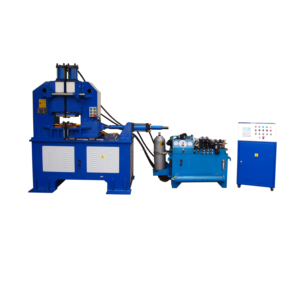
Delivering high-reliability fusion equipment to infrastructure projects globally
When global infrastructure projects require high-integrity polymer fluid handling systems or continuous metal wire forming, selecting a premier China Best Butt Welder Supplier is a critical engineering decision. Butt welding technology—encompassing both thermoplastic heat fusion (HDPE, PP-R, PVDF) and metal electrical resistance flash butt welding—serves as the backbone for gas distribution, municipal water mains, chemical processing networks, and automotive structural frame manufacturing.
Modern industrial procurement officers cannot evaluate suppliers solely on capital cost. Achieving joint integrity that exceeds the tensile strength of the base material requires strict adherence to international standardizations such as ISO 21307 (Plastic pipes and fittings — Butt fusion jointing procedures), DVS 2207-1 (Welding of thermoplastics), and ASTM F2620. A top-tier manufacturer integrates precise hydraulic proportional valves, PTFE-coated heating elements with digital PID loop controllers, dynamic planar facing tools, and automated data-logging telemetry.
Technical Insight: A high-quality butt fusion joint relies on controlling four core thermodynamic parameters: Heating Plate Temperature ($T$), Drag Pressure ($P_d$), Interfacial Heat Soak Pressure ($P_1$), and Joint Cooling Time under Clamp Pressure ($T_c$). Elite suppliers calibrate hydraulic output down to $\pm 0.05 \text{ MPa}$ to prevent polymer degradation and stress concentration rings.
Industrial buyers frequently navigate two distinct technology branches when evaluating butt welding machinery suppliers:
Utilizes a heated aluminum matrix coated in non-stick PTFE to melt polymer pipe ends, followed by controlled hydraulic butt pressing to achieve complete molecular chain entanglement.
Employs high-current electrical arc flashing to burn off wire/rod end face irregularities, followed by a high-tonnage forge stroke to join metal rings and frames instantly.
Integrates precision servo-driven wire bending arm mechanisms directly with in-line butt resistance heads for 2D/3D high-speed frame manufacturing.
Compare operational limits across machine classes to match your project bill of materials (BOM):
| Welder Classification | Pipe/Wire Capacity | Automation Grade | Primary Material Focus | Field Mobility Rating |
|---|---|---|---|---|
| Portable Manual 2-Ring | 50mm – 200mm | Manual / Hand Crank | HDPE, PE, PP, PB | High (Lightweight Trench Work) |
| Hydraulic Station (Medium) | 90mm – 355mm | Semi-Automatic Hydraulic | PE100, PP-R, PVDF | Medium (Skid Mount / Trailer) |
| Heavy Mega-Pipe Hydraulic | 630mm – 1200mm | Electro-Hydraulic Proportional | Thick-Wall Mining & Gas HDPE | Stationary / Truck-Mounted |
| 2D 4-Axis CNC Engine | 2mm – 6mm Wire Rod | Fully Automated CNC Servo | Stainless Steel, Iron Wire Frame | Factory Floor Stationary |
| Heavy Flash Butt (UN Series) | Up to 200KVA Output | Pneumatic/Hydraulic Flash Forge | Steel Rings, Wheel Rims, Bars | Heavy Production Line |
As global pipeline engineering transitions toward smart infrastructure and zero-defect compliance, China's manufacturing sector is pioneering several critical advances in butt welder production:
GPS-enabled hydraulic stations automatically record time, heating temperature, drag pressure, and ambient humidity. Welding parameters are transmitted directly to project quality dashboards via 4G/5G telemetry to prevent manual falsification.
Adopting ASTM F2620 High-Pressure standards allows jointing at 0.52 MPa instead of traditional low-pressure 0.17 MPa. This cuts total cooling cycle times by up to 50%, accelerating pipeline laying speeds dramatically.
Replacing heavy low-frequency transformers with IGBT solid-state inverters reduces machine power consumption by 30% while offering microsecond electrical pulse control during flash-butt metal joining.
Leveraging over 44 years of specialized welding domain expertise since 1980, our partner facilities maintain rigorous ISO 9001 quality management across the entire manufacturing lifecycle. Each machine undergoes exhaustive multi-point stress testing before factory dispatch:
Continuous 24-hour pressure holding test at 1.5x max rated pressure to ensure zero internal valve leakage.
High-precision thermal imaging scans ensure $\pm 2^\circ\text{C}$ temperature uniformity across heating plates.
Sample pipe weld joints undergo 180-degree bend tests and tensile pulling until pipe wall failure occurs.
CNC-milled aluminum inserts engineered to custom pipe outer diameters (OD) and wall thicknesses (SDR).
Whether you require field-ready HDPE fusion machines, heavy mega-pipeline hydraulic stations, or custom CNC wire forming equipment, our engineering sales team is ready to deliver factory-direct quotes and technical consultation.