

Knowledge Hub & Insights
Knowledge Hub & Insights
Engineered for extreme duty cycles, structural integrity, and multi-process versatility. Designed for global export with full international compliance.
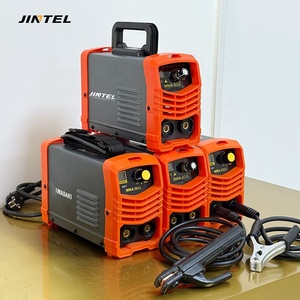
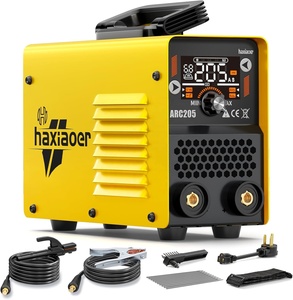
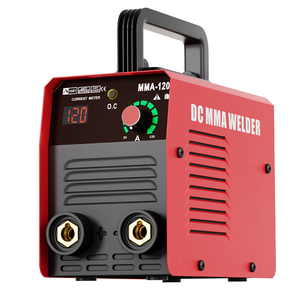
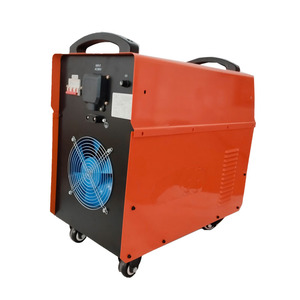
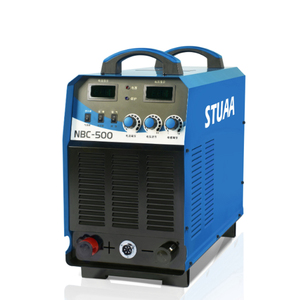
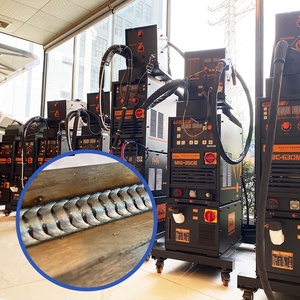
Tungsten Inert Gas (TIG) welding, dynamically categorized as Gas Tungsten Arc Welding (GTAW), remains the gold standard for high-precision joint integrity, corrosion-resistant metallurgy, and visually flawless bead profiles. For industrial procurement directors and engineering managers navigating cross-border supply chains, sourcing from a direct CE Certified TIG Welder Manufacturer & Exporter guarantees that power electronics, electrical safety, electromagnetic compatibility, and duty-cycle ratings adhere strictly to harmonized European Norms (EN 60974-1 and EN 60974-10).
Modern industrial TIG manufacturing has shifted definitively from legacy transformer architectures to IGBT (Insulated Gate Bipolar Transistor) High-Frequency Inverter Topology. This technological leap enables digital switching frequencies exceeding 20 kHz to 100 kHz, drastically reducing internal core mass while delivering instantaneous arc response, precise pulse wave modulation, and exceptional energy efficiency (Power Factor > 0.93).
Founded in 1980 in the GIDC Industrial Estate at Vatva, Ahmedabad, India, Parag Electrodes Agencies Pvt. Ltd. (Paragweld) has established itself as a premier engineering power in the manufacture and global export of heavy-duty industrial welding equipment, electrodes, and digital inverter power sources.
Operating with an unyielding commitment to metallurgical perfection, our manufacturing infrastructure combines automated SMT board assembly, rigorous high-voltage insulation vacuum impregnation, and environmental chamber testing to ensure uninterrupted operation under severe ambient conditions (-20°C to +55°C).
CE LVD (2014/35/EU) & EMC (2014/30/EU) certified, guaranteeing low harmonic distortion and safe insulation.
Tailored dual-voltage transformers, custom duty-cycle configurations (up to 100% @ 400A), and private-label casing.
100% burn-in testing, artificial dust chamber exposure, and oscilloscopic arc stability profiling on every production line.
When welding exotic alloys—such as AISI 316L stainless steel, Inconel 625, or 6061-T6 aerospace aluminum—the primary challenge is managing Heat-Affected Zone (HAZ) expansion while maintaining complete root penetration and preventing heat warping or burn-through. Advanced CE-certified TIG power sources utilize digital microprocessor controls to shape output waveforms with microsecond precision:
Aluminum naturally forms a tough, high-melting-point (2,072°C) oxide film ($Al_2O_3$) that prevents proper fusing of the base metal (which melts at only 660°C). Our AC TIG welders incorporate adjustable AC Balance Control (20% to 80% EN). The Electrode Positive (EP) half-cycle blasts away oxide layers via cathodic cleaning action, while the Electrode Negative (EN) half-cycle concentrates heat into the workpiece for deep penetration.
By alternating rapidly between a high Peak Current ($I_p$) and a lower Background Current ($I_b$) at pulse frequencies ranging from 0.5 Hz up to 500 Hz, operators achieve pinpoint arc stiffness. High pulse frequencies compress the plasma column, increasing arc force while reducing overall net heat input by up to 45%, making thin-gauge sheet metal fabrication effortless and warp-free.
| Technical Parameter | Legacy Transformer TIG | Standard Inverter TIG | Advanced CE Digital Pulse TIG |
|---|---|---|---|
| Inverter Frequency | 50 / 60 Hz | 20 kHz - 40 kHz | 100 kHz IGBT Soft-Switch |
| Power Efficiency | 60% - 68% | 80% - 85% | 92% - 95% (Energy Star Compliance) |
| Arc Ignition Mechanism | Scratch / High Loss HF | Standard HF / Lift TIG | Micro-Controlled Clean HF / Non-HF Lift |
| Pulse Frequency Range | None (Static Current) | 0.5 Hz - 20 Hz | 0.5 Hz - 500 Hz Ultra-Fast |
| Duty Cycle @ Rated Max | 35% @ 40°C | 60% @ 40°C | 60% - 100% Industrial Heavy Duty |
As industrial procurement shifts toward smart factories, carbon-neutral manufacturing, and supply chain transparency, global buyers must evaluate vendor capabilities against four major long-term market trends:
Top-tier aerospace, defense, and nuclear energy fabricators require full traceability for every weld seam. Modern TIG welders are increasingly equipped with Ethernet/Wi-Fi modules and RS485 Modbus protocols that record real-time voltage, amperage, gas flow rate, and heat input parameters directly into Enterprise Resource Planning (ERP) or Manufacturing Execution Systems (MES) to guarantee Welding Procedure Specification (WPS) compliance.
International electrical codes (such as EN 61000-3-12) are enforcing stringent harmonic current distortion limits. European and North American buyers are prioritizing TIG welders featuring active Power Factor Correction (PFC) modules. PFC enables stable welding across extended cable runs (up to 100 meters) and wide supply voltage fluctuations (90V - 275V) while reducing line current draw by over 30%.
Faced with global skilled welder shortages, manufacturing enterprises are rapidly deploying Collaborative Robots (Cobots) for TIG welding tasks. Forward-thinking procurement officers choose TIG power sources equipped with digital interface cards (DeviceNet, Profinet, Analog 0-10V) that allow full remote control of arc ignition, current ramps, and filler wire feeding directly from a robotic controller.
Eliminating intermediary broker markups is crucial for heavy equipment buyers. Sourcing directly from established Indian manufacturing hubs—such as Paragweld in Vatva, Ahmedabad—provides a major cost advantage while ensuring robust export logistics, including CE Conformity Certificates, Certificates of Origin (Form A/AFTA), and comprehensive spare parts supply kits.
The future of GTAW power sources is heavily anchored in solid-state power semiconductor advancements and intelligent micro-gas dynamics. Key technological developments engineered into our upcoming machinery generations include:
Replacing standard silicon IGBTs with next-generation Silicon Carbide (SiC) transistors enables ultra-high switching frequencies exceeding 200 kHz, delivering zero electrical noise, near-instantaneous arc response, and a 40% reduction in thermal dissipation losses.
Advancing deep-penetration single-pass welding up to 10mm thickness in titanium, stainless steel, and nickel alloys without requiring edge beveling or filler wire, radically boosting structural output speeds by up to 800%.
Proportional electronic gas valve controls automatically scale argon/helium shielding gas pre-flow and post-flow durations according to real-time welding amperage and torch temperature, cutting expensive gas consumption by up to 35%.
Comprehensive answers to essential technical and purchasing questions for international machinery importers, distributors, and engineering contractors.
Looking to upgrade your manufacturing facility or expand your machinery distribution network? Request our comprehensive industrial catalog, complete CE technical compliance documentation, and factory-direct B2B wholesale pricing.