

Knowledge Hub & Insights
Knowledge Hub & Insights
Explore our certified range of manual arc welders, heavy-duty MIG/MAG inverter machinery, multi-process synergy units, high-capacity submerged arc automatic systems, and 6-axis robotic arms. Engineered for international standards compliance (EN 60974-1, CE Machinery Directive 2006/42/EC), each unit delivers maximum arc stability, thermal endurance, and duty cycle efficiency.
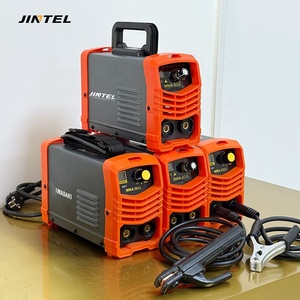
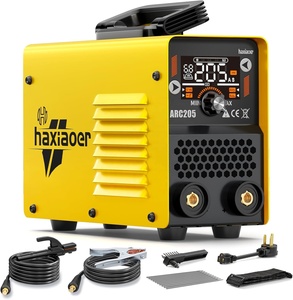
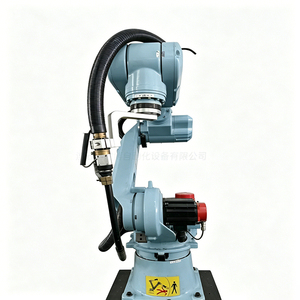
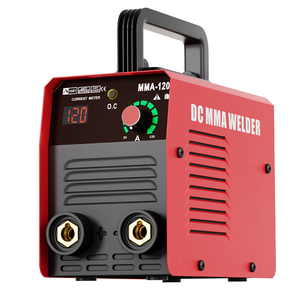
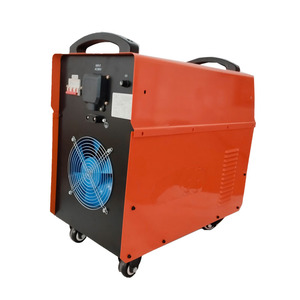
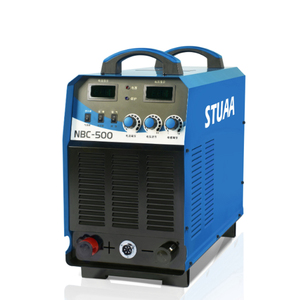
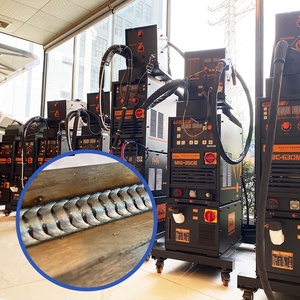
Founded in 1980 by Mr. Parag Mashruwala in the heart of GIDC Vatva, Ahmedabad, Gujarat, India, Parag Electrodes Agencies Pvt. Ltd. (Paragweld) has established itself over four decades as a premier manufacturer, supplier, and direct global exporter of industrial welding machines, air plasma cutters, submerged arc auto welders, and heavy-duty stick electrodes.
Serving heavy manufacturing sectors including structural steel fabrication, forging plants, metal casting shops, shipbuilding yards, and pressure vessel fabricators, Paragweld combines deep metallurgical knowledge with advanced electrical engineering. Every CE-certified welding and cutting system is tested under full thermal overload conditions to guarantee zero-defect operational deployment for international B2B purchasers.
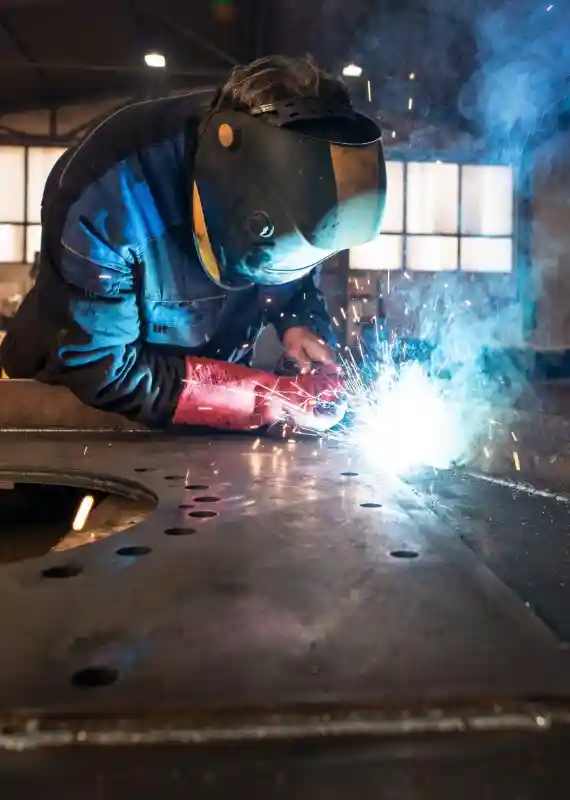
State-of-the-Art Production Facility in GIDC Vatva & Founder Mr. Parag Mashruwala
The global industrial sector is undergoing a rapid transition toward energy-efficient, digitally controlled, and highly automated metal joining and cutting equipment. As industrial procurement teams evaluate global suppliers, understanding the technological shifts from traditional transformer-rectifier units to high-frequency IGBT (Insulated Gate Bipolar Transistor) and SiC (Silicon Carbide) power architectures is vital to optimizing Total Cost of Ownership (TCO) and long-term operating profitability.
Modern CE certified cutting and welding machines rely on advanced IGBT modules capable of switching frequencies exceeding 20 kHz to 50 kHz. This high-frequency operation drastically reduces the mass of the magnetic core transformer, resulting in machines that are 70% lighter while achieving an electrical efficiency conversion rate of over 85%.
Traditional manual voltage adjustments are increasingly replaced by synergy microprocessors. Synergic control algorithms automatically calculate optimal wire feed speed, peak current, background current, and pulse frequency based on selected base metal thickness, shielding gas mixture (e.g., Ar/CO2 blends), and wire diameter (0.8mm to 1.6mm). This eliminates operator error, drastically reduces spatter rate by up to 65%, and ensures consistent weld bead geometry across multi-shift fabrication lines.
With persistent skilled welder shortages globally, high-volume production facilities in shipbuilding, structural steel fabrication, and automotive frame construction are standardizing on 6-axis articulated welding robotic arms. Robotic cells integrated with digital pulse MIG/MAG power sources achieve travel speeds up to 150 cm/min with near-zero weld defect rates. Advanced bus communication protocols (Profinet, EtherCAT, CANopen) allow seamless handshake between robot controllers and welding power sources for fully automated factory environments.
Strategic guidance for procurement officers, plant directors, and OEM buyers navigating international equipment sourcing.
Regulatory scrutinization is intensifying across European and North American markets. Importers must verify that factories provide authentic CE compliance documentation, including EN 60974-1 (Arc Welding Equipment), Low Voltage Directive 2014/35/EU, and RoHS directives, shielding buyers from costly customs impounds and liability claims.
Industrial electricity costs account for over 60% of total lifetime operating costs of heavy duty welders. Procurement decision-makers are actively replacing legacy transformer welders (45%-55% efficiency) with high-efficiency IGBT inverters (>85% efficiency) to achieve corporate Scope 2 decarbonization targets.
Instead of purchasing standalone units for separate welding and cutting tasks, multi-process power sources capable of performing Gas Metal Arc Welding (GMAW), Shielded Metal Arc Welding (SMAW), Lift TIG, and Air Plasma Cutting inside one rugged power chassis are becoming the preferred CapEx investment for job shops.
Global supply chain vulnerabilities have led buyers to favor certified export factories like Paragweld that maintain robust spare parts inventory (IGBT modules, printed circuit boards, drive rollers, torches) and guarantee long-term technical support to eliminate unexpected factory downtime.
Comparative specification grid engineered to assist industrial engineers in specifying correct power source topologies.
| Technology Category | Primary Process | Output Current Range | Duty Cycle Rating | Typical Target Substrates | CE Standard Compliance |
|---|---|---|---|---|---|
| Portable Inverter MMA | Manual Arc (SMAW) | 20A - 300A | 60% @ 300A | Carbon Steel, Stainless, Rebar | EN 60974-1 / CE / ISO9001 |
| Synergy Dual Voltage | MIG/MAG / ARC / TIG | 30A - 205A | 60% @ 205A | Sheet Metal, Auto Body, Stainless Steel | EN 60974-1 / EMC Directive |
| Robotic Arc Arm System | Automated MIG/MAG/TIG | up to 500A Continuous | 100% Continuous | Structural Beams, Heavy Pressure Vessels | CE Machinery Directive 2006/42/EC |
| Industrial Heavy Duty ZX7 | High-Amperage SMAW | 60A - 630A | 60% @ 630A | Heavy Alloy Plates, Gouging, Structural | EN 60974-1 / LVD 2014/35/EU |
| Submerged ARC (SAW) | Submerged Automatic Arc | 200A - 1250A | 100% Continuous | Boiler Shells, Wind Towers, Ships | EN 60974-1 / Heavy Industrial CE |
| Air Plasma Cutter Series | Thermal Plasma Arc Cut | 30A - 200A | 60% to 100% | Mild Steel, Stainless, Aluminum Alloys | CE / ISO Quality System Verified |
Addressing key technical, compliance, and logistics questions raised by international machinery buyers and engineering contractors.
CE certification indicates that the cutting or welding equipment complies with essential European health, safety, and environmental protection regulations. Specifically for industrial power sources, CE marking ensures adherence to EN 60974-1 for electrical safety, the Low Voltage Directive (2014/35/EU), and the EMC Directive (2014/30/EU) for electromagnetic interference. Non-compliant machinery risks being confiscated by customs authorities and poses severe electrical hazards to factory operators.
Duty cycle is a standardized measure (defined over a 10-minute test period at 40°C ambient temperature) indicating how long a machine can operate continuously at a specific current before overheating. A machine rated 60% at 500 Amps can weld continuously for 6 minutes at 500A, requiring 4 minutes of fan cooling. For continuous automated production lines (such as robotic welding cells or submerged arc seam welding), a 100% duty cycle rating is required to eliminate thermal thermal-cutout interruptions.
IGBT (Insulated Gate Bipolar Transistor) inverter machines utilize high-frequency switching technology to convert AC mains power to DC, reducing transformer core mass by over 70%. In comparison to heavy copper transformer units, IGBT inverters provide 30-40% lower power consumption, superior dynamic arc response, precise digital control over pulse parameters, and lightweight portability, resulting in significantly lower electricity expenses and higher weld quality.
Yes. Many Paragweld models feature smart auto-sensing dual-voltage input circuitry (e.g., 110V/220V single-phase or 380V/415V three-phase). Built-in microprocessors automatically detect grid voltage and adjust primary transformer taps, protecting sensitive control electronics against harmful voltage sags, spikes, and phase imbalances commonly encountered in industrial job sites and remote generator power grids.
Paragweld implements a 100% multi-stage testing procedure at its manufacturing facility in GIDC Vatva, Ahmedabad. Protocols include high-voltage insulation dielectric testing, extended thermal burn-in under maximum current load, oscilloscopic waveform arc verification, and structural drop/vibration stress testing. Each unit is dispatched with a factory test inspection certificate and user documentation detailing operating limits.
Submerged ARC Welding (SAW) uses a granular fusible flux to completely cover the arc during welding. This process eliminates UV radiation and weld spatter while delivering exceptionally high deposition rates (up to 15 kg/hr per arc wire). SAW provides deep joint penetration, making it the ideal process for longitudinal and circumferential seams on heavy pressure vessels, structural H-beams, wind turbine towers, and ship hulls.
Paragweld has a dedicated international export department with over 40 years of experience serving clients across 30+ countries. We handle complete export documentation, seaworthy wooden crate packaging, and customs clearance support. For after-sales technical support, we maintain a comprehensive stock of critical spare parts (IGBT modules, control PCBs, wire feeder drives, plasma torches) dispatched via express air freight, supported by remote video troubleshooting with our senior electrical engineers.
We offer comprehensive OEM/ODM manufacturing partnerships for global distributors and equipment brands. Customization options include custom chassis colorways, brand labeling, custom dynamic front-panel digital displays, tailored duty-cycle transformer windings, specialized input voltage configurations (such as 575V for Canadian markets), and localized operator manuals.